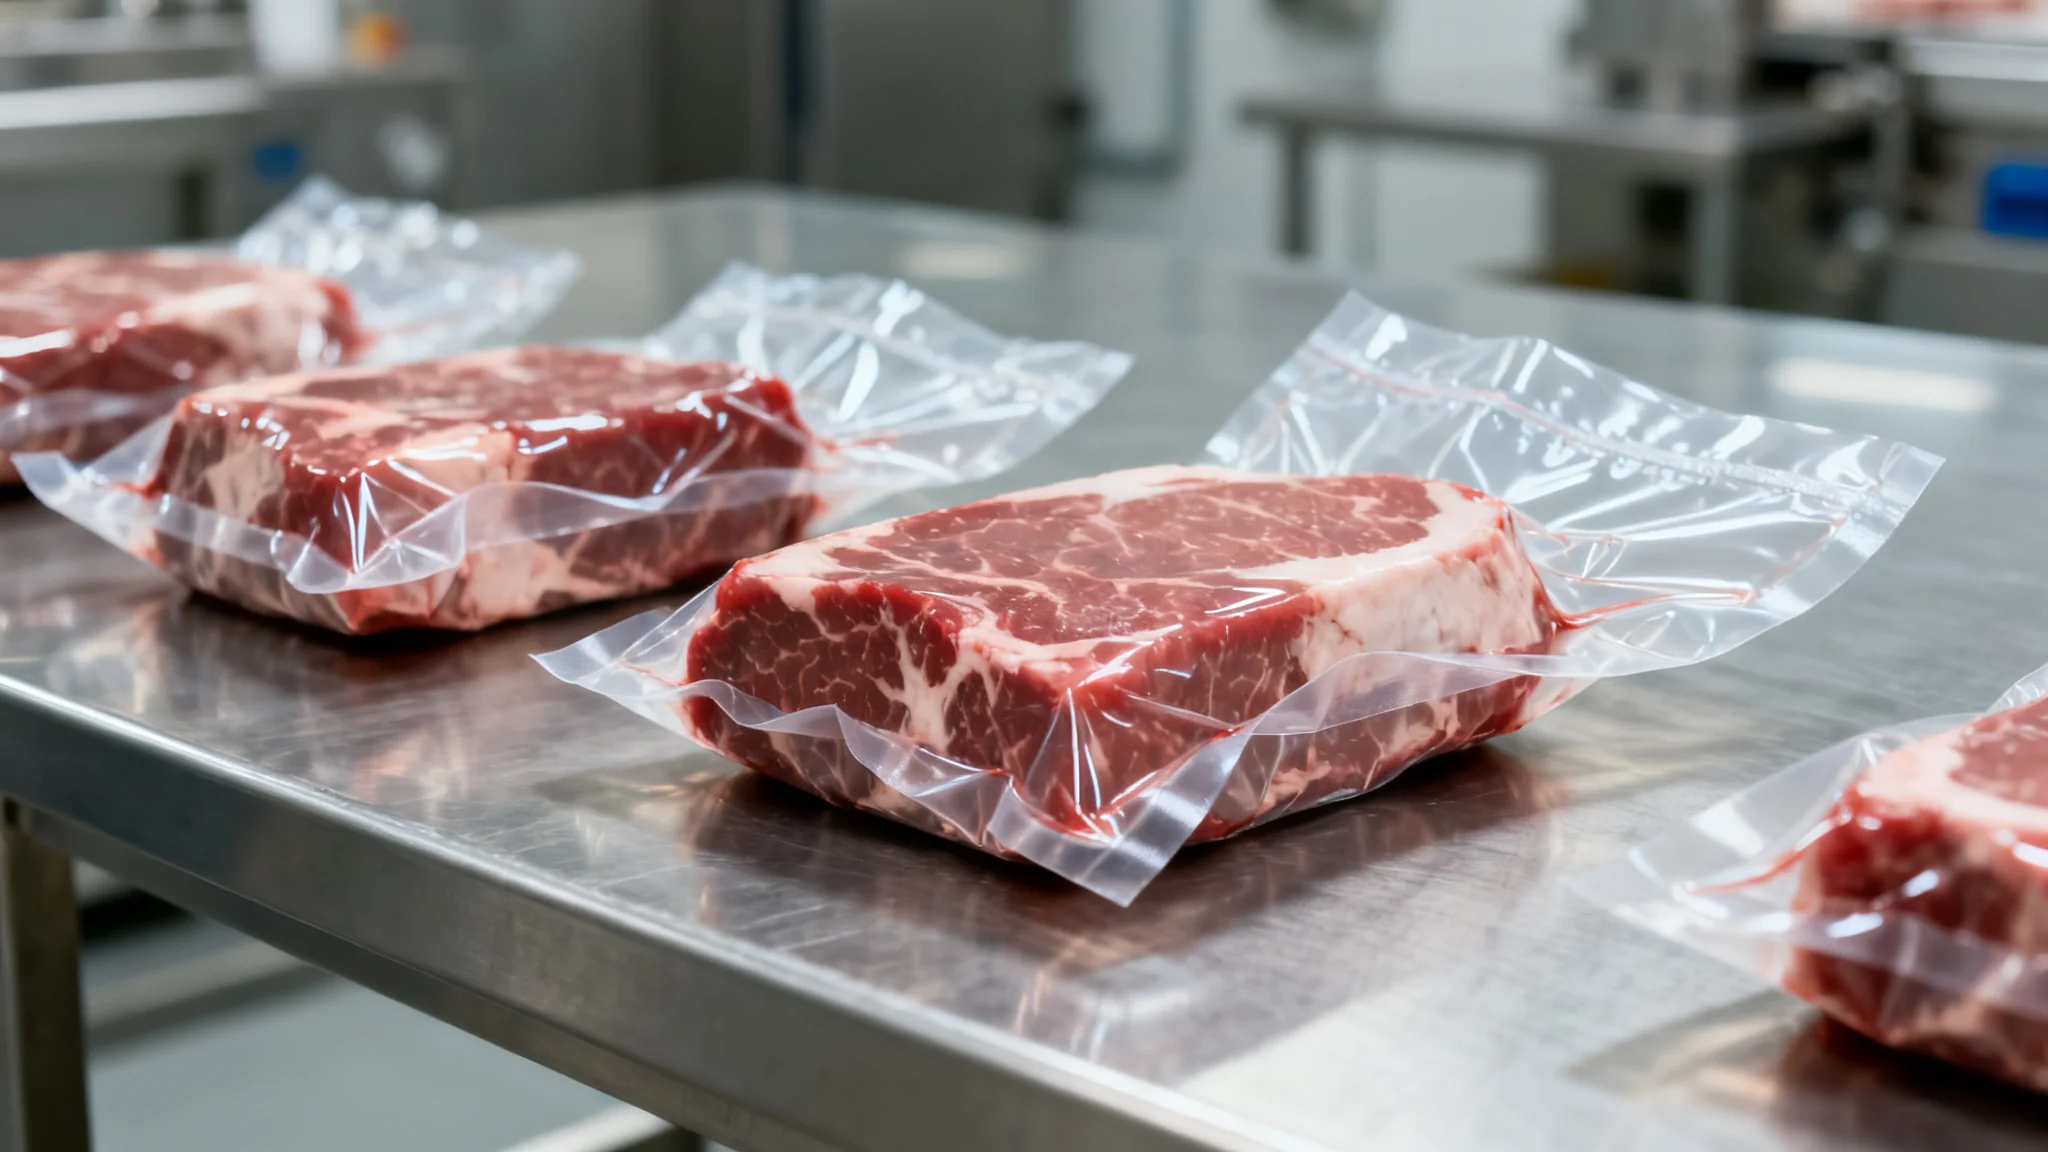
Fragile snack packaging usually breaks at the seal or at the puncture point, not in the middle of the film. That single observation changes the troubleshooting order, because chasing a thicker film first is expensive and often leaves the real cause untouched. This article is written for packaging engineers, quality staff and buyers who need to find out why breakage and leakage appear after filling or after transport, and who want a sequence that separates film causes from seal causes and from handling causes.
Symptoms That Point to Different Causes
The first useful step is to record when the failure appears, because the timing narrows the cause before any material is tested. Four patterns cover most of what arrives as a breakage complaint:
- Fails at the jaw, passes at the customer. The bag looks sound at the end of the line and loses pressure within days. This points to creep in a marginal seal, or to a seal that was still warm when it was handled.
- Fails along one line of the fin. A channel rather than a burst, often with product debris or print inside the seal zone. Look at the filler and the film surface before the material grade.
- Fails at a fold or a corner. A single puncture with a clean edge, usually where the bag bends against the case. This is a geometry and stiffness question as much as a film question.
- Fails in the product, not the pack. The bags arrive intact and the snack is broken. Work on compression, fill volume and case configuration instead of the film.
Key Takeaways
- Locate the failure position on real returned packages before testing any material.
- A thicker film helps only when the failure is a puncture or a stiffness problem, not when it is a seal channel or an overfilled case.
- Seal strength results are comparable between suppliers only when the test method and its conditions are stated.
Where Does the Break Actually Happen?
Locate the failure on the package, not in the batch. Open a set of returned bags, find the physical position of the leak or tear, and mark it. Position tells you which machine station or which handling event is implicated far more reliably than any single test result.
Two positions deserve attention because they are easy to miss. The first is the crease where the bag folds against the carton wall, which is often intact when the bag sits flat and fails when it is compressed. The second is the area just inside the end seal, where internal pressure is highest and where a small contamination point grows into a slow leak.
Which Film Properties Matter for Fragile Snacks?
Three properties carry most of the load for a fragile snack: puncture resistance, stiffness and barrier. Puncture resistance decides whether a sharp edge inside the bag turns into a hole. Stiffness decides how the bag distributes a compressive load instead of bending at one point. Barrier decides how long the product survives once the pack is sealed.
These properties can pull against each other. The nylon film grades used for puncture resistance bring moisture sensitivity of their own, which changes how the structure behaves in a humid warehouse and how it must be laminated. Specifying the property that fixes the visible complaint, without checking the side effects, is how a breakage problem turns into a barrier problem.
Is It the Seal or the Film?
Separate the two with a controlled sequence rather than an opinion. Take bags from the same production run, and separate them into three groups: as produced, held under compression, and held under compression after a temperature cycle. A seal defect tends to appear in the held and cycled groups while the as-produced group stays tight. A film defect tends to appear in the as-produced group as well.
When the evidence points to the structure rather than the process, the next decision is about format and material combination. The flexible packaging product ranges set out how those combinations are normally grouped, and the sampling route for a change of this kind is described under our packaging services, which is where a specification change should start rather than on the production line.
What Puncture Resistance Does Not Tell You
Puncture resistance describes a test coupon, not a finished bag. The value depends on the film thickness at the test point, the shape and radius of the probe, and the speed of the test. A number measured with a rounded probe on a flat sample does not describe what happens when a sharp fragment presses into a crease on a filled, pressurised bag.
Two limits matter in practice. The result is directional: a laminate can resist a puncture from the sealing layer and fail from the print side. It is also a single-point event, while a bag in a case meets repeated low-level compression that the test does not simulate. Treat the value as a screening property, and test the finished package as a unit.
The Troubleshooting Order
Work through these steps in order, and stop as soon as the evidence points clearly at one cause:
- Locate the failure position on a set of real returned packages, and record how many fail at each position.
- Confirm the leak or break is repeatable by holding the packages under compression for a defined period.
- Check the seal window against the actual line speed, including cooling time before handling.
- Inspect the seal zone for debris, print or lacquer contamination from the product and the film.
- Only then compare material options, using coupons cut from production film rather than a supplier sample.
- Re-run the original distribution test on the changed package before releasing the new specification.
Why Test Numbers Do Not Travel Between Labs
Seal strength is a commonly quoted number, and it is commonly compared between suppliers who measured different things. The test specimen, the support span, the peel angle, the crosshead speed and the conditioning time all change the result, so two numbers measured under different conditions cannot be ranked against each other.
The way to keep the comparison honest is to state the method alongside the value. ASTM F88/F88M covers seal strength of flexible barrier materials and fixes those conditions, which is what makes a result repeatable between two sites. For loss of package integrity rather than seal peeling, ASTM F2096 describes gross leak detection by internal pressurisation, a bubble test that answers a different question: does the finished package hold pressure at all.
When Breakage Is Not a Packaging Problem
Some breakage complaints sit outside the scope of the laminate. If the bags arrive intact and the product inside is broken, the cause sits in fill volume, case fill rate, stacking height or the route itself. If the product contains a hard fragment, such as a nut piece or a hard-baked inclusion, the puncture risk is a product property and the structure has to be chosen around it.
Metallised and foil-containing structures are often proposed for this situation, and they do raise barrier, but thin metal layers have their own failure mode. The pinhole behaviour of aluminium foil laminates is a good example: the material improves one property while adding a crease-sensitive weakness that only appears in the finished bag.
Conclusion
Start by locating where the package fails, and only then decide whether the cause is the seal, the film or the handling route. A thicker film will not close a channel that runs along a seal, and a tighter seal will not protect a product that is being crushed in an overfilled case. Where the evidence does point to the structure, change one variable at a time and confirm the result with a distribution test on the packed case, using a stated test method so the outcome can be compared later.
Frequently Asked Questions
Why does breakage show up after transit rather than at the packing line?
Transit adds repeated low-level compression, vibration and temperature change to packages that were only inspected once, at the end of the line. A marginal seal creeps open over days instead of failing at once, and a fold pressed against a case edge concentrates strain on one line. The result is a package that passes a short factory check and fails later. Reproducing those inputs means holding samples under compression for a defined period, and running the packed case through a defined distribution cycle rather than testing loose bags. A fragile snack packaging specification should record those conditions next to the seal value.
Does a thicker film always reduce snack breakage?
No. Thickness helps only when the failure is a puncture or a stiffness problem, and it does nothing when the cause is a seal channel, an overfilled case or a stacking height that exceeds what the pack can carry. Adding gauge also raises the load on the seal in some structures, so a thicker film can move the failure rather than remove it. Identify the failure position first, and treat a gauge change as one option among several, to be confirmed by retesting.
How do you tell a seal leak from a film puncture?
Use position and behaviour together. A seal leak tends to follow the fin or the end seal, and it usually appears or grows after the package is held under compression or after a temperature cycle. A puncture has a visible entry point at a fold, a corner or the point where a hard fragment presses inward, and it appears in a single location rather than along a line. Separating as-produced, compressed and cycled samples shows which of the two you have before any material is changed.
What should a transit test include for fragile snacks?
Test the packed case, not loose bags, and apply a defined sequence of hazards rather than a single drop. Compression under a static load, random vibration and a drop at a corner or edge cover most of what a carton meets in distribution. Record the units per case and the stacking height with the result, because both change the load the packages carry. Repeat the same sequence whenever fill volume, case configuration or film gauge changes, so the comparison stays valid.