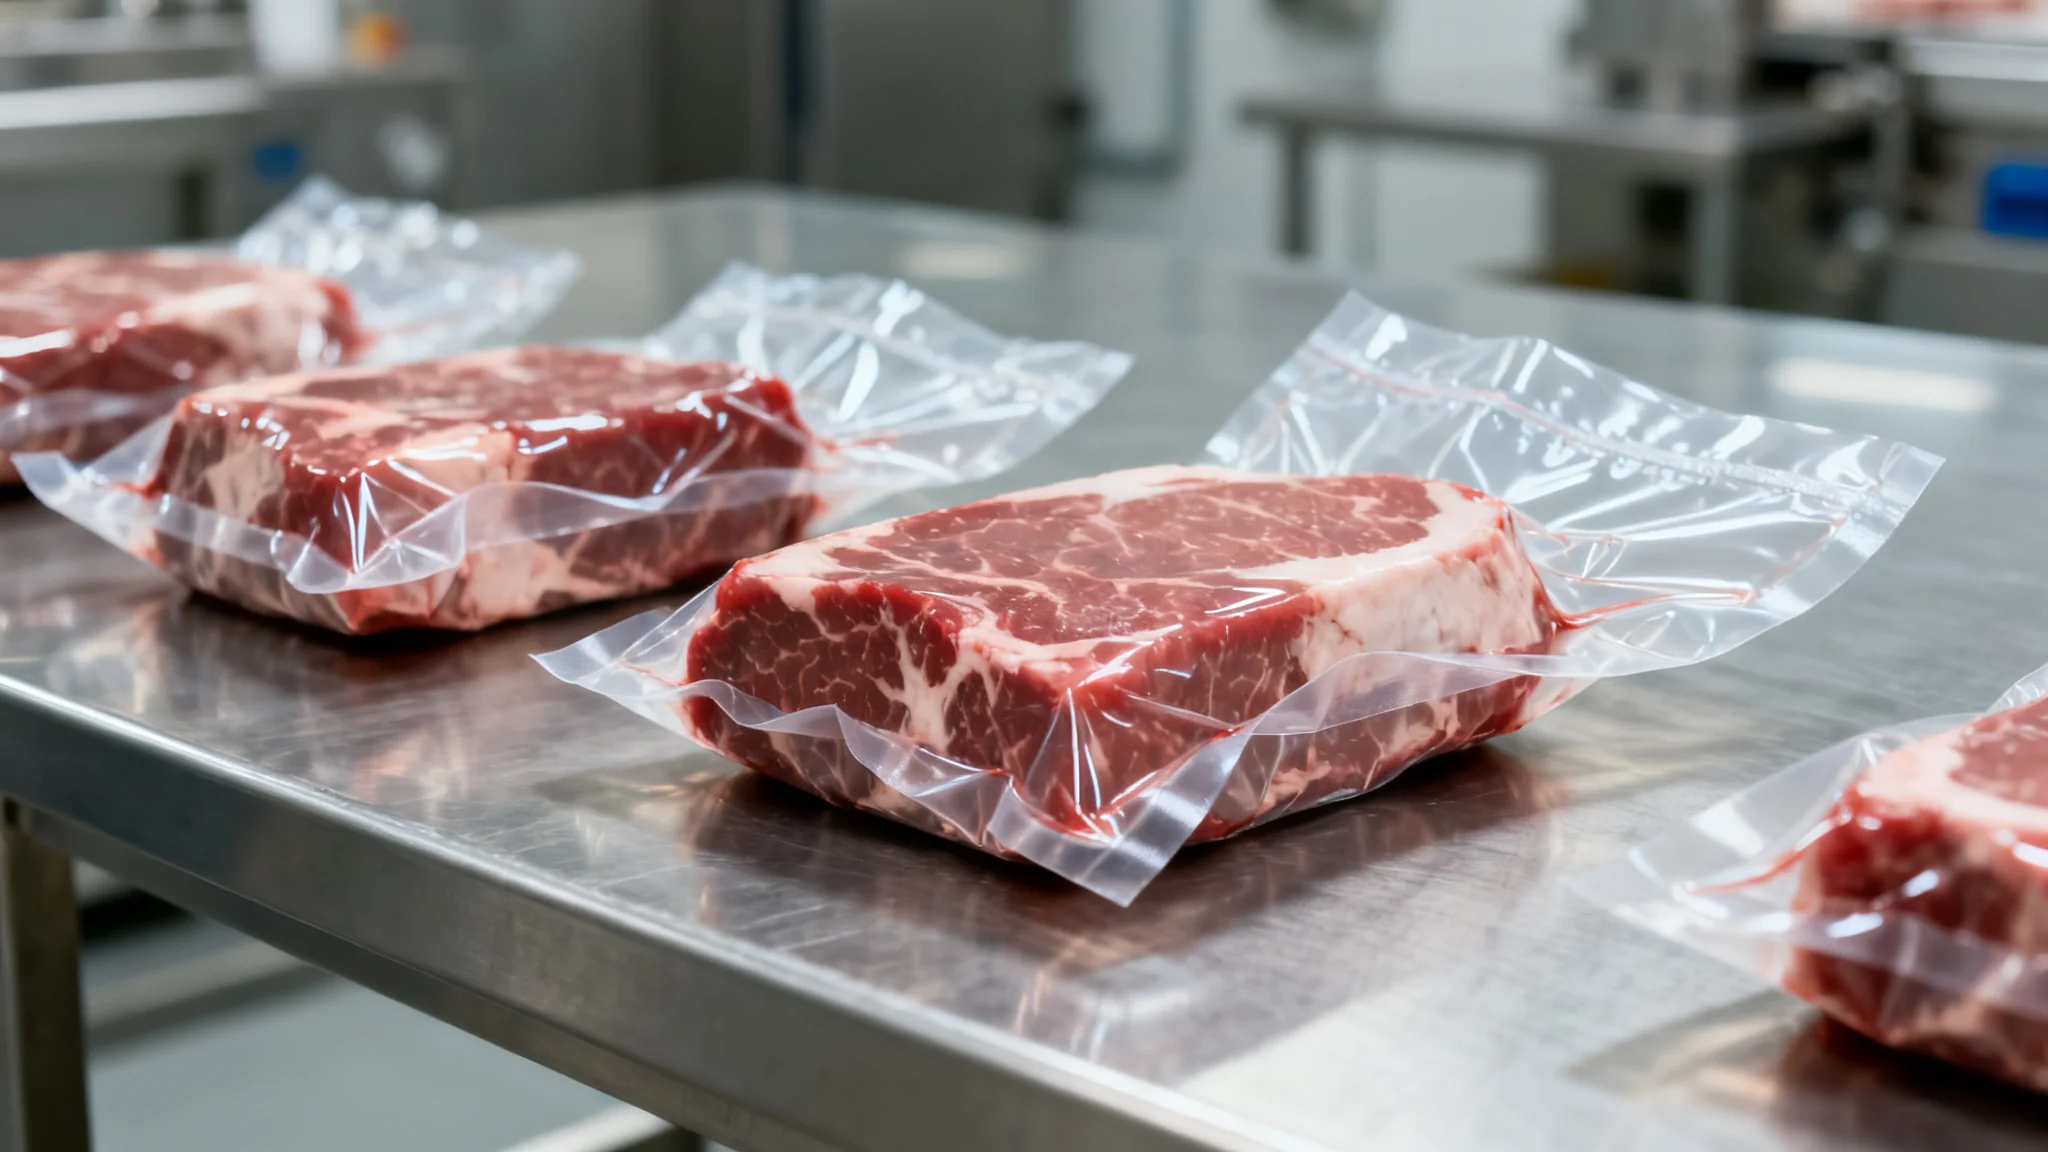
Frozen vegetable packaging fails from the inside out before it fails from the cold. Frost collects in the headspace, the film fogs, and a pack that sealed cleanly at filling starts to show ice crystals along the seam after a week in the freezer. The cause is usually moisture that was never given a place to go, combined with a pack line running in conditions the film was not trialled for. This article works through venting, frost and cold-room line effects in the order they appear on the line.
Key Takeaways
- Frost inside a pack is trapped moisture, not a material defect; it comes from surface water, product moisture and humid headspace air.
- Venting trades frost against moisture loss, so it belongs to a trial rather than to a fixed specification.
- Cold rooms change both film tracking and machine behaviour, and one set of seal parameters rarely covers room and cold conditions.
- Hold trial packs long enough for frost to form, then run a leak test on frozen packs rather than on warm film.
Why frozen produce packs fog and frost from the inside
Frost inside a pack is condensed moisture, and it arrives from three places: free surface water left on the product after washing, moisture the product releases as it equilibrates, and humid air trapped in the headspace at filling. Sealing traps all three. As the pack cools, that moisture condenses on the coldest surface available, which is usually the film facing the freezer air.
Fogging and frost are separate problems. Fogging is a surface effect on the inside of the film, and anti-fog additives reduce it for the consumer. Frost is water that has already condensed and frozen, and it forms at the seam, in the corners and around product edges. You can reduce fog and still have a frost problem, so check them separately on the trial packs.
How much venting does a frozen vegetable pack actually need?
Venting helps when the product still respires or when the pack traps humid air that has nowhere to escape. It hurts when the product needs protection from moisture loss or freezer burn. The right amount is not a fixed figure; it depends on surface moisture, respiration after blanching, pack size and how long the pack sits in the cold chain.
Blanched frozen vegetables respire far less than fresh produce, so the venting question sits closer to moisture management than to respiration. Small perforations or a micro-perforated film give headspace moisture an exit, but they also create a path for moisture loss in dry freezer air. That trade-off is why venting belongs to a trial rather than to a specification sheet.
Which pouch format suits which frozen produce line?
Format follows handling more than product type. A pillow pack on a vertical form-fill-seal line suits free-flowing vegetables at high speed, and it is the cheapest route per unit. A stand-up pouch suits retail packs that sit on a shelf or in a freezer drawer, and it needs more headspace for the bottom gusset. Rollstock on a horizontal line suits flat, regular shapes.
The decision usually turns on three things: how the product feeds, how fast the line runs, and how the pack is displayed and opened. A format that fills perfectly can still fail if the gusset traps product during filling, so check the fill station as carefully as the film. Retail frozen vegetable bags and similar formats are a useful reference point for how the produce packaging bags are structured for this category.
What changes on a pack line running in a cold room?
Cold rooms change film behaviour and machine behaviour at the same time. Film becomes stiffer, so it tracks differently through the forming collar and seals less easily at the same jaw temperature. Lubricants thicken, sensors drift, and belts that ran cleanly at room temperature can slip.
Operators often respond by raising seal temperature. That helps up to a point, then it causes the film to thin at the seam or to stick to the jaws. A better sequence is to slow the line slightly, confirm the film is being pulled straight, and only then adjust temperature and pressure. If the same structure is filled at both room and cold-room temperature, run the trial under both, because one set of parameters rarely covers both.
How do you verify frost and seal performance before a full run?
Freeze the trial packs the way the chain will freeze them, then hold them long enough for frost to form rather than judging them the next morning. Inspect the seam, the corners and the area where product touches film, because that is where condensation collects. Open a sample and look for ice inside the seal, not just on the film surface.
For seal integrity, a bubble or dye test on frozen packs shows leaks that a peel test can miss, and a standard such as ASTM F2096 gives a repeatable reference. Water vapour transmission data measured to ASTM F1249 is useful for ranking films, though it describes the film rather than the finished pack. Freezer burn is mostly a moisture-loss problem rather than a safety one, and extension material on why freezer burn happens is a reasonable background source for explaining it to a sales team.
Where this applies and where it does not
This applies to frozen vegetables and similar produce filled on a normal pack line and held in a standard commercial freezer chain. They apply less well to individually quick frozen product that is packed in bulk liners, to packs that are gas-flushed for a specific retail requirement, and to lines where the product is frozen after packing rather than before.
They also assume the freezer is the main environment. If a pack travels through a humid ambient stage, for example a port with high humidity during transloading, the condensation risk shifts and the venting answer can change.
Trial checklist for a frozen produce line
- Record fill weight, product surface moisture and product temperature at the fill station.
- Run the film at production speed in the actual room temperature, not a warm test bay.
- Freeze the samples the way the chain freezes them and hold long enough for frost to develop.
- Check the seam, the corners and the product contact area for trapped ice.
- Run a leak test on frozen packs, then confirm the structure before buying the next reel.
Trade-offs between venting and barrier
More venting means less trapped moisture and less frost, but also more moisture loss in dry freezer air and a shorter shelf life for products that oxidise. A high-barrier film protects the product but holds in any moisture that was sealed inside. Most frozen vegetable packs land somewhere between the two, and the right point depends on how long the pack is expected to sit in the chain.
Cold-chain length is often underestimated. A pack designed for a short regional route can behave differently on a long export route with several transfers, even when the product and format are the same.
Which faults point to film, and which point to the line?
Diffuse frost across the film usually points to moisture in the product or the headspace. Localised frost around the seam points to the seal or the fill station. Torn film at a corner points to handling or to a gusset that traps product. Grouping the fault by where it appears saves a lot of guessing, because the same visible symptom can come from the film or from the machine.
Conclusion
Frost, fog and seal problems in frozen vegetable packaging are moisture and line-condition questions before they are material questions. Trial the structure in the real cold room, hold the samples long enough for frost to appear, and check seal integrity on frozen packs. Confirm the format against the fill station as well as the film, and review the interaction with custom packaging built for frozen products where the same moisture behaviour appears in a different format.
Frequently Asked Questions
Does frozen vegetable packaging need perforations?
Only when headspace moisture or residual respiration has nowhere else to go. Blanched vegetables respire little, so perforations are mainly a moisture-management tool, and they also let moisture escape into dry freezer air. Test perforated and unperforated film on the real product, compare frost at the seam and weight loss after storage, and keep the variant that holds up over the full shelf-life period rather than in a single shift.
Why does frost form at the seal even when the pack looks dry?
Because the moisture that matters is often invisible at filling. Humid air in the headspace, or a thin film of surface water left on the product, condenses at the coldest point as the pack cools, and the seam is usually that point. Check the fill station for product entering the seal area, and hold trial packs long enough for frost to develop before judging whether the frozen vegetable packaging performs as expected.
Can the same film run at room temperature and in a cold room?
Rarely with the same machine settings. Stiff film tracks differently and seals less easily when cold, so jaw temperature, pressure and line speed usually need separate values for each condition. Run the trial in both environments rather than transferring settings, note which values changed, and then check the seal on frozen packs before writing the parameters into the line standard.
How long should trial packs be held before checking for frost?
Long enough for the pack to pass through a real cooling cycle and develop condensation, which is normally several days rather than overnight. Judge frost at the seam, in the corners and around product contact points, and combine that with a leak test on frozen packs. Review the wider material options in low-temperature freezing packaging materials before locking the structure.